Do you have any tips on determining ROI to justify an investment in online elemental analysis?
Justifying any decision around online analysis requires careful and fair consideration of the associated upside.
For a decision around dedicated sampling/analysis stations for a new build, we recommend making a conservative estimate of savings in materials and not underestimating the value of time. A few months' saving on the construction timeline translates directly into an earlier swing from expenditure to income, an inflection point that cannot come soon enough for most projects.
For process control, consider the current situation to determine the magnitude of possible gains. For example:
- What is a recovery improvement worth for your process?
- If you could reduce impurities in the concentrate, what would that mean for selling price?
- What’s the difference in flotation reagent consumption, best to worst current case? What would be the savings if you consistently hit the best case?
- How much are you overmilling over milling to avoid overly coarse material exiting the grinding circuit? What would be the energy savings if you weren’t? Online analysis should pay its way, and easily, so calculations such as these should readily highlight optimal areas for economic implementation and provide evidence to support investment.
How does real-time online elemental analysis data assist in stabilizing grinding circuit and flotation plant operations?
In the grinding circuit, under-grinding typically means poor metal recovery (mineral processing) or sub-standard product (cement). Over-grinding, on the other hand, drives up energy consumption and results in undesirable levels of fines. Milling just enough, balances these competing impacts. Online real-time particle sizing analysis makes it possible both to identify an optimal setpoint for particle size and then reliably maintain it.
In a flotation plant, there is an analogous balance to establish. Poor separation means excessive metal loss while excessive reagent addition is expensive and environmentally undesirable. Here, real-time elemental analysis can provide the information needed to identify the operational sweet spot and optimal control in the face of changes in particle size, ore mineralogy, and pulp density.
In both cases, with real-time data, changes tend to be more frequent but smaller, i.e., the plant stabilizes, with automated control minimizing variability.
Why is high availability of assay data necessary for effective process control in elemental analysis?
If you are aiming for automated process control, then that is only practical with high availability and 95% should be an absolute minimum. Otherwise, switching to and from manual process control will be arduous and problematic with respect to operational efficiency. If availability is not demonstrably high, then operators cannot rely on an analyzer, whether control is manual or automated, and it never becomes an integral part of the control architecture.
How important is measurement interval for process control with on-line elemental analyzer data? How can I determine how often to sample/measure?
When implementing online analysis, there are two key questions to consider: What can I measure? And what can I control to affect that measurement?
Let’s take grinding circuit control as an example. A measurable variable is the particle size of the exiting material, and it can be controlled by parameters such as mill throughput and speed of rotation. How often to measure is then the next question. With manual control, a large interval between measurements inhibits an operator’s ability to adjust the process effectively. There is a long lag between taking action and seeing the result. Increasing measurement frequency, to the limit of real-time measurement, improves feedback allowing the operator to learn how to 'steer' the circuit more effectively. The result will be steadier operation with an automated, well-tuned control loop, the best solution for driving variability to a minimum.
If you can measure and tightly control a vital characteristic of a key stream, in a grinding or flotation circuit, or elsewhere on the plant, then the rewards can be substantial. If you can’t influence a measurable parameter, then there is far less impetus to measure it at all, or with any frequency, though measurement may still be valuable for upset monitoring. Focus on how you would use data if you had it to identify the best places for investment and the frequency of measurement that will be most useful.
What are the operational pros and cons of multi-stream and dedicated analyzers for slurries?
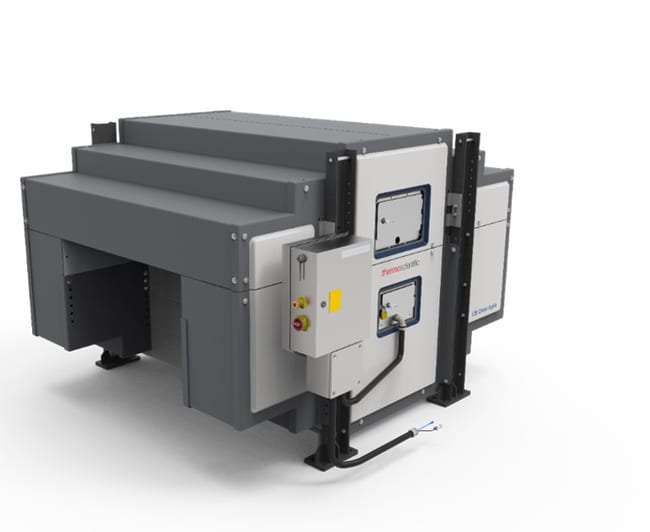
Well-designed dedicated analyzers require only minimal cleaning and maintenance for reliable operation over the long-term. The sample transport associated with centralized systems, on the other hand, requires the addition of pumps and small-bore sample lines adding additional complexity and failure points to the system. These have potential to affect data availability and cost of ownership due to the maintenance, running costs, and emissions associated with pump operation. Such systems are often installed with good intentions and a sound understanding of the practice required to keep them in good working order, but over the years, enthusiasm and rigor have tended to dwindle. Abandoned lines are common with centralized analyzers, an important point to note when assessing upfront CAPEX.
The other significant difference between multi-stream and dedicated analyzers is measurement frequency. For streams that justify real-time measurement, or as close as is feasible, dedicated analyzers are unbeatable.